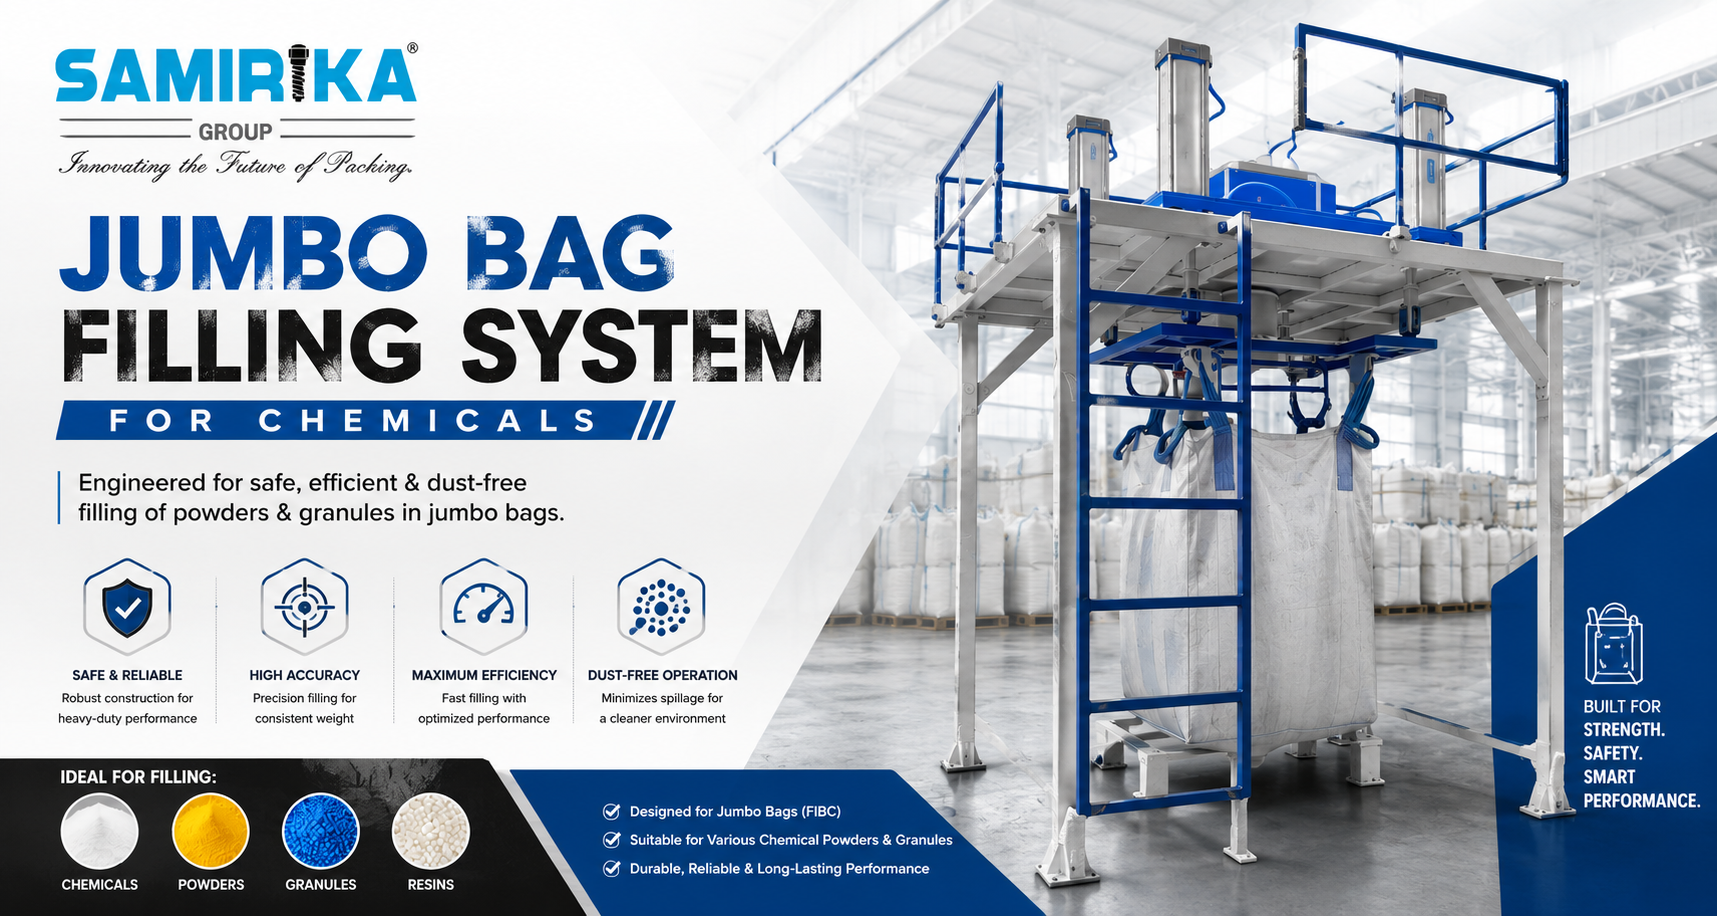
Jumbo Bag Filling System for Chemicals
Enhance chemical handling efficiency with a robust Jumbo Bag Filling System. Discover features, applications, and selection criteria for Ahmedabad industries.
Why This Matters in Ahmedabad
Ahmedabad, a vibrant industrial hub in Gujarat, hosts a significant number of chemical manufacturing and processing units. The region's robust infrastructure and thriving industrial ecosystem necessitate efficient material handling solutions. Companies dealing with bulk chemicals, whether powders, granules, or flakes, face constant pressure to optimize their packaging operations. A reliable Jumbo Bag Filling System directly addresses these needs by improving throughput, reducing operational costs associated with manual labor and product wastage, and ensuring compliance with stringent safety regulations prevalent in the chemical sector.
What is a Jumbo Bag Filling System for Chemicals — Overview
A Jumbo Bag Filling System for Chemicals is an automated or semi-automated piece of industrial equipment designed to accurately and efficiently fill large bulk bags (FIBCs) with various chemical products. These systems typically incorporate features for bag handling, filling, weighing, and discharge. For chemical applications, they are constructed with materials resistant to corrosion and chemical reactions, and often include dust containment or extraction systems to manage airborne particles. The core function is to precisely dispense a predetermined weight or volume of chemical into an FIBC, preparing it for storage, transport, or further processing.
Key Features and Technical Specifications
- Robust Construction: Built with corrosion-resistant materials like stainless steel (SS304, SS316) or specialized coatings to withstand aggressive chemical environments.
- Accurate Weighing System: Integrated load cells and advanced controllers for precise weight dispensing, ensuring product integrity and compliance.
- Dust Containment: Features such as dust skirts, collection hoods, or integrated dust extraction ports to minimize airborne particulate matter.
- Bag Handling Mechanism: Automated or semi-automated systems for positioning, inflating, and securing the FIBC neck onto the filling spout.
- Variable Filling Rates: Adjustable flow control to accommodate different product densities and flow characteristics, preventing bridging or excessive dust generation.
- Safety Interlocks: Built-in safety features to prevent operation unless the bag is properly positioned and secured, and to stop the system in case of anomalies.
- Programmable Logic Controller (PLC): User-friendly interface for setting fill weights, managing recipes, and monitoring system performance.
- Optional Features: Integration with palletizers, conveyors, or other downstream packaging equipment for a complete automated line.
Industrial Applications and Use Cases
- Fertilizer Packaging: Filling bulk bags with granular or powdered fertilizers for agricultural distribution.
- Petrochemical Handling: Packaging various polymer pellets, resins, or additives in large quantities.
- Specialty Chemical Dispensing: Accurately filling FIBCs with fine chemicals, pigments, or catalysts.
- Mineral and Ore Processing: Packaging bulk minerals, ores, or construction chemicals like cementitious powders.
- Food Grade Chemical Packaging: Filling ingredients or additives for the food processing industry under strict hygiene standards.
- Detergent and Cleaning Agent Production: Packaging powdered or granular cleaning agents in bulk.
- Pharmaceutical Intermediates: Filling bulk intermediates for the pharmaceutical sector where precision is paramount.
How to Choose the Right Jumbo Bag Filling System
Selecting the appropriate system is crucial for optimizing your chemical packaging operations. Consider these key factors:
- Product Characteristics: Analyze the physical properties of your chemical – particle size, density, flowability, abrasiveness, and corrosiveness. This dictates material selection and filling mechanism.
- Required Throughput: Determine the number of bags you need to fill per hour or shift to match your production demands.
- Accuracy Requirements: Understand the tolerance for weight variation. Higher accuracy is critical for high-value or regulated chemicals.
- Safety and Environmental Standards: Ensure the system meets local and international safety regulations for chemical handling, including dust control and explosion prevention if applicable.
- Integration Needs: Consider if the system needs to interface with existing equipment like conveyors, palletizers, or automated guided vehicles (AGVs).
- Supplier Expertise and Support: Choose a manufacturer with proven experience in the chemical industry and a strong track record for after-sales service and spare parts availability.
- Customization Options: Assess if the system can be tailored to specific plant layouts, product variations, or unique operational requirements.
Quality Standards and Compliance
For chemical applications, adherence to quality standards and regulatory compliance is non-negotiable. Systems should be designed and manufactured to meet relevant industry standards. This often includes using food-grade or chemical-resistant materials as specified by standards like those from the International Organization for Standardization (ISO). For systems handling potentially hazardous materials, compliance with ATEX directives (for explosive atmospheres) or similar regional safety standards is vital. Buyers should verify that the manufacturer can provide documentation and certifications demonstrating compliance with these critical quality and safety benchmarks.
Why Samirika Industries Pvt. Ltd. Experience and Capability Matters
Samirika Industries Pvt. Ltd. brings a wealth of experience in designing and manufacturing material handling and automation solutions tailored for demanding industrial environments. Our expertise in the chemical sector means we understand the unique challenges associated with handling corrosive, abrasive, or sensitive materials. We leverage precision engineering and robust manufacturing processes to build systems that are not only efficient but also exceptionally durable. Our technical team possesses deep knowledge of automation controls and material flow dynamics, enabling us to offer customized solutions that precisely meet your operational needs.
We are committed to rigorous quality control throughout our manufacturing process, ensuring that every Jumbo Bag Filling System for Chemicals leaving our facility adheres to the highest standards of performance and safety. Our capability extends to integrating these systems seamlessly into your existing production lines, providing comprehensive support from initial consultation through installation and after-sales service. This holistic approach ensures you receive a reliable, high-performing solution designed for long-term operational excellence.
Installation, Maintenance and Care Tips
Proper installation and regular maintenance are key to the longevity and optimal performance of your Jumbo Bag Filling System.
- Installation: Ensure the system is installed on a level, stable surface. Connect all electrical and pneumatic lines according to the manufacturer's specifications. If dust extraction is included, ensure it is properly ducted and functional.
- Initial Setup: Calibrate the weighing system with certified test weights to ensure accuracy. Program fill weights and other operational parameters through the PLC interface.
- Daily Checks: Before operation, inspect the bag clamping mechanism for wear, check seals for integrity, and ensure all safety guards are in place.
- Regular Cleaning: After each batch or shift, clean the filling spout and surrounding areas to prevent product buildup and cross-contamination. Use appropriate cleaning agents compatible with the system's materials.
- Preventative Maintenance: Schedule periodic inspections of load cells, pneumatic components, and wear parts. Lubricate moving parts as recommended in the operation manual.
- Calibration: Re-calibrate the weighing system regularly, especially after any maintenance or if accuracy drifts are observed.
- Spare Parts: Keep a stock of critical wear parts, such as seals, gaskets, and pneumatic components, to minimize downtime during unexpected failures.
Frequently Asked Questions
The system is designed to handle a wide range of chemical products, including powders, granules, pellets, and flakes. Material compatibility is ensured through the use of corrosion-resistant construction materials like stainless steel, making it suitable for both general and specialized chemical applications.
Accuracy is achieved through high-precision load cells integrated into the weighing system, coupled with sophisticated PLC controls. These systems monitor the weight in real-time and automatically adjust the filling rate to achieve the target fill weight with minimal deviation.
Safety features typically include robust dust containment systems to minimize airborne particles, interlocks that prevent operation if the bag is not properly secured, and options for explosion-proof components if handling flammable materials. Emergency stop buttons are also standard.
Yes, most systems are designed to accommodate a range of standard FIBC sizes. Adjustments for different bag dimensions, such as neck height and width, can usually be made through simple mechanical adjustments or programmable settings.
With proper installation, regular maintenance, and adherence to operating guidelines, a well-built Jumbo Bag Filling System can have a lifespan of 10-15 years or more. The durability of the construction materials and the quality of the components significantly influence its longevity.
Samirika Industries Pvt. Ltd. provides comprehensive after-sales support, including installation assistance, operator training, preventative maintenance programs, and readily available spare parts. Our technical team is also accessible for troubleshooting and ongoing operational support.
Conclusion
For chemical manufacturers and processors in Ahmedabad and across Gujarat, a reliable Jumbo Bag Filling System for Chemicals is a critical investment in efficiency, safety, and product integrity. By understanding the specific characteristics of your chemical products, your throughput requirements, and the available technological features, you can select a system that not only meets but exceeds your operational expectations. Partnering with an experienced manufacturer like Samirika Industries Pvt. Ltd. ensures you receive a robust, precisely engineered solution backed by expert support, empowering your business to achieve new levels of productivity and operational excellence in the competitive chemical industry.
Get In Touch
Samirika Industries Pvt. Ltd.