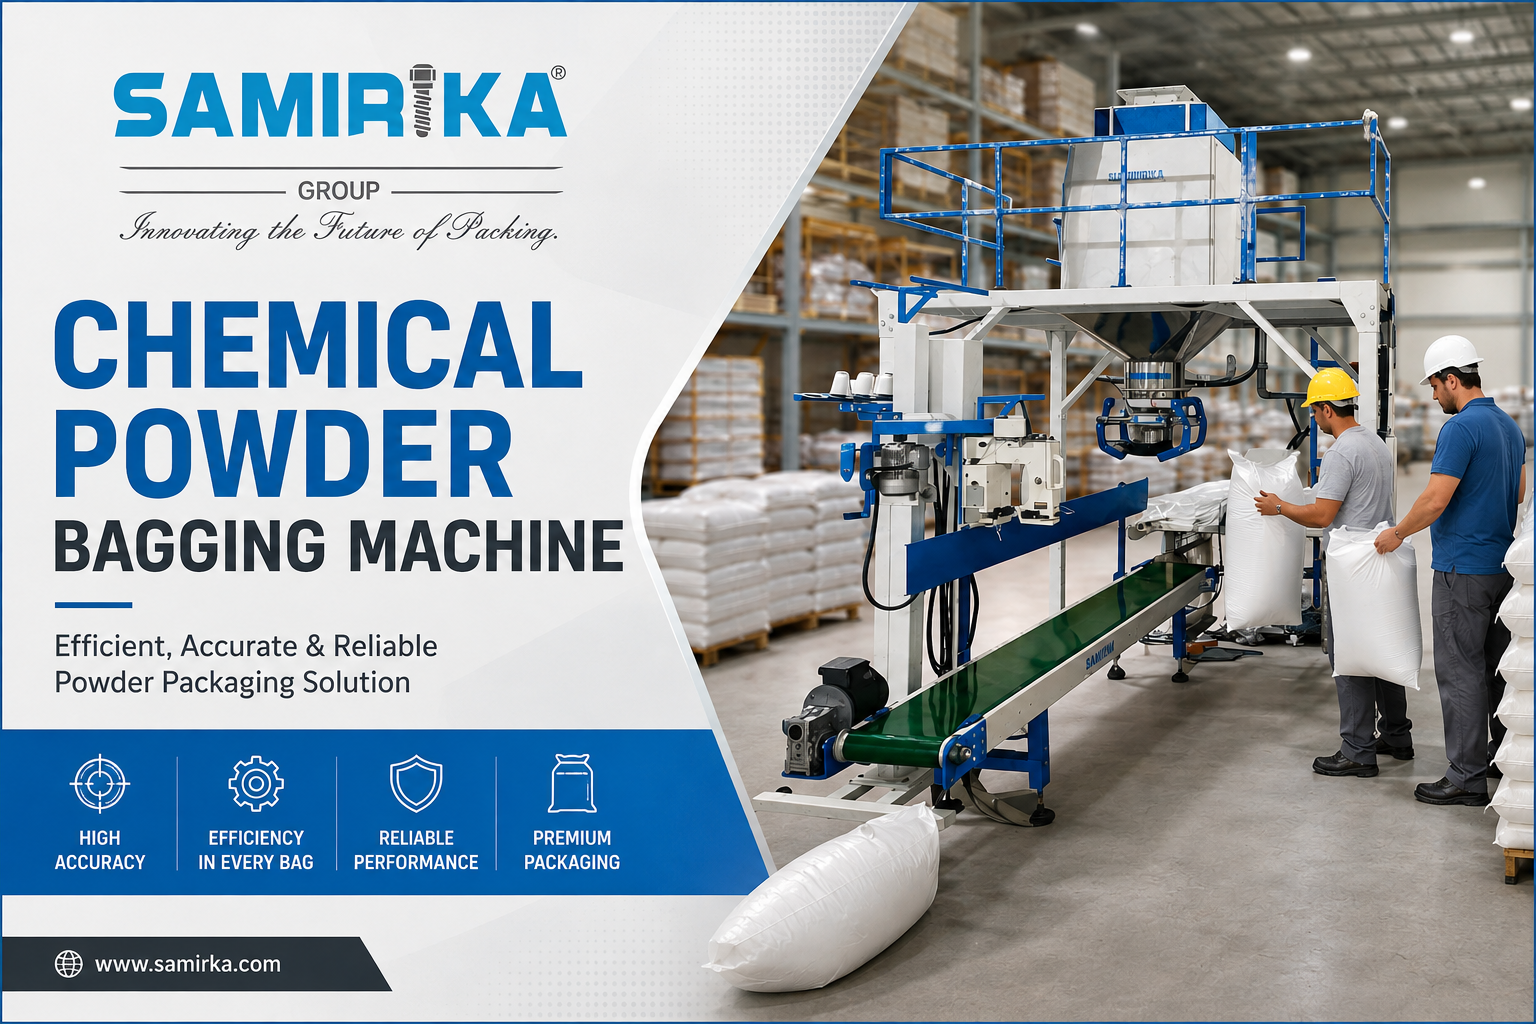
Chemical Powder Bagging Machine
Expert chemical powder bagging machine solutions in Ahmedabad. Enhance efficiency and accuracy with Samirika Industries' automated systems.
Key Features and Technical Specifications
When evaluating a chemical powder bagging machine, several key features contribute to its performance and suitability for your specific needs:
- Accurate Dosing System: Utilizes auger fillers or vibratory feeders for precise powder dispensing, ensuring consistent fill weights within tight tolerances.
- Dust Containment: Integrated dust collection systems and sealing mechanisms to minimize airborne particles, protecting workers and the environment.
- Bag Handling Versatility: Capable of handling various bag types, including pre-made bags, gusseted bags, and stand-up pouches, in different materials like plastic, paper, or woven polypropylene.
- High-Speed Operation: Designed for efficient throughput, capable of bagging a significant number of units per minute or hour.
- User-Friendly Interface: Microprocessor-based controllers with touchscreens for easy operation, parameter setting, and monitoring of the bagging process.
- Robust Construction: Built with durable materials, often stainless steel, to withstand the corrosive or abrasive nature of certain chemical powders and ensure longevity.
- Safety Features: Incorporates emergency stop buttons, safety guards, and interlocks to protect operators during operation.
- Customization Options: Ability to adapt fill weights, bag sizes, and sealing methods to meet specific product and market requirements.
Industrial Applications and Use Cases
The versatility of chemical powder bagging machines makes them essential across numerous sectors within the chemical industry and beyond:
- Fertilizer Production: Packaging granular and powdered fertilizers for agricultural use, ensuring accurate nutrient delivery.
- Detergent Manufacturing: Filling bags with powdered laundry detergents, dishwashing powders, and industrial cleaning agents.
- Pigment and Dye Packaging: Accurately bagging powdered pigments and dyes used in paints, textiles, and plastics, with attention to color integrity and dust control.
- Food Additives and Ingredients: Packaging powdered food additives, spices, flour, and other ingredients under hygienic conditions.
- Pharmaceutical Powders: Filling bags with bulk pharmaceutical powders and active pharmaceutical ingredients (APIs) where precision and sterility are paramount.
- Construction Chemicals: Packaging powdered admixtures, cement additives, and grouts.
- Agrochemicals: Bagging powdered pesticides, herbicides, and other crop protection chemicals.
- Resins and Polymers: Filling bags with powdered resins and polymer additives used in manufacturing.
How to Choose the Right Chemical Powder Bagging Machine
Selecting the appropriate chemical powder bagging machine requires careful consideration of your operational needs and product characteristics. Use this checklist to guide your decision:
- Product Characteristics: Assess the powder's flowability, particle size, density, abrasiveness, and tendency to clump or generate dust. This will determine the most suitable filling mechanism (auger, vibratory, etc.) and dust control features.
- Bag Type and Size: Identify the specific types of bags you will use (e.g., flat, gusseted, stand-up) and their dimensions. Ensure the machine can handle these and achieve a secure seal.
- Required Throughput: Determine the number of bags you need to fill per hour or shift to match your production volume and meet market demand.
- Accuracy Requirements: Understand the acceptable tolerance for fill weight. High-value or regulated products demand higher accuracy.
- Dust Control Needs: Evaluate the level of dust containment required based on safety regulations, environmental concerns, and product value.
- Automation Level: Decide between a fully automatic system for high-volume production or a semi-automatic option for smaller batches or more specialized tasks.
- Material Compatibility: Ensure the machine's construction materials are compatible with the chemicals being bagged to prevent corrosion or contamination.
- Supplier Support: Consider the availability of installation, training, maintenance, and spare parts from the manufacturer or supplier.
Quality Standards and Compliance
For chemical powder bagging machines, adherence to quality standards and regulatory compliance is non-negotiable. Buyers should verify that the equipment meets relevant industry benchmarks. This often includes certifications like ISO 9001 for quality management systems, demonstrating the manufacturer's commitment to consistent product quality. Depending on the specific chemicals being handled and the target markets, compliance with standards related to food-grade materials (if applicable), hazardous material handling, or environmental protection (like dust emission limits) may also be necessary. Verifying the machine's design for safety, ease of cleaning, and material traceability is crucial for ensuring both operational integrity and regulatory adherence.
Why Samirika Industries' Experience and Capability Matters
At Samirika Industries Pvt. Ltd., our extensive experience in material handling and automation solutions, particularly for the chemical sector in Ahmedabad, sets us apart. We understand the intricate demands of packaging diverse chemical powders, from fine dusts to granular materials. Our manufacturing processes are geared towards precision engineering, ensuring that each chemical powder bagging machine we deliver is robust, reliable, and built to last.
Our technical team possesses deep expertise in designing systems that offer exceptional accuracy, efficient dust containment, and user-friendly operation. We pride ourselves on our capability to customize solutions, tailoring machines to the unique specifications of your product and production line. This commitment extends to rigorous quality control throughout the manufacturing cycle, guaranteeing that our equipment meets the highest standards of performance and durability. Choosing Samirika Industries means partnering with a provider dedicated to enhancing your operational efficiency and product integrity.
Installation, Maintenance, and Care Tips
Proper installation, regular maintenance, and diligent care are vital for the optimal performance and longevity of your chemical powder bagging machine.
- Installation: Ensure the machine is installed on a stable, level surface in a well-ventilated area. Connect all utilities (power, compressed air if applicable) according to the manufacturer's specifications. Proper calibration of the weighing system is critical at this stage.
- Daily Checks: Before operation, visually inspect the machine for any loose parts, wear, or damage. Check that safety guards are in place and functional.
- Cleaning: Regular cleaning is essential, especially when switching between different products or batches. Follow the manufacturer's recommended cleaning procedures to prevent cross-contamination and maintain hygiene. Pay close attention to the filling mechanism and sealing jaws.
- Lubrication: Periodically lubricate moving parts as per the maintenance schedule to ensure smooth operation and prevent premature wear.
- Calibration: The weighing system should be recalibrated regularly to maintain fill accuracy. The frequency will depend on usage and product consistency.
- Wear Parts: Keep an eye on wear parts such as sealing jaws, belts, and filler components. Replace them proactively before they fail to avoid production downtime.
- Preventive Maintenance: Schedule periodic preventive maintenance checks with qualified technicians. This can help identify potential issues before they become major problems.
- Operator Training: Ensure all operators are thoroughly trained on the machine's operation, safety features, and basic maintenance procedures.
Frequently Asked Questions
A1: Modern chemical powder bagging machines, especially those with auger fillers and advanced weighing systems, can achieve very high accuracy, typically within ±1% to ±2% of the target fill weight. The exact accuracy depends on the powder's characteristics, the machine's design, and proper calibration.
A2: These machines are designed to handle a wide range of powders, including fine powders, granular materials, and even some sticky or cohesive substances. The specific type of filler (auger, vibratory) and features like dust control are selected based on the powder's properties.
A3: Effective dust control is achieved through integrated dust collection hoods, vacuum systems that capture airborne particles at the filling point, and well-sealed bag filling and sealing mechanisms. Proper machine design and regular maintenance of these components are crucial.
A4: Many chemical powder bagging machines are designed with versatility in mind. They can often be adjusted or equipped with change parts to accommodate a range of bag sizes and types, including pre-made bags, gusseted bags, and stand-up pouches.
A5: Routine maintenance includes daily cleaning, regular lubrication of moving parts, periodic calibration of the weighing system, and inspection of wear parts like sealing jaws. Preventive maintenance by trained technicians is also recommended.
A6: Safety features commonly include emergency stop buttons, safety interlocks on access doors, overload protection for motors, and guards around moving parts to prevent operator injury.
Conclusion
For chemical manufacturers and processors in Ahmedabad, investing in a high-quality chemical powder bagging machine from a trusted provider like Samirika Industries Pvt. Ltd. is a strategic decision. It directly impacts operational efficiency, product quality, worker safety, and regulatory compliance. By carefully considering product characteristics, required throughput, bag specifications, and the supplier's expertise, you can select a system that not only meets your current needs but also supports your future growth. Samirika Industries is committed to delivering robust, accurate, and reliable bagging solutions tailored to the unique challenges of the chemical industry.
Get In Touch
Samirika Industries Pvt. Ltd.