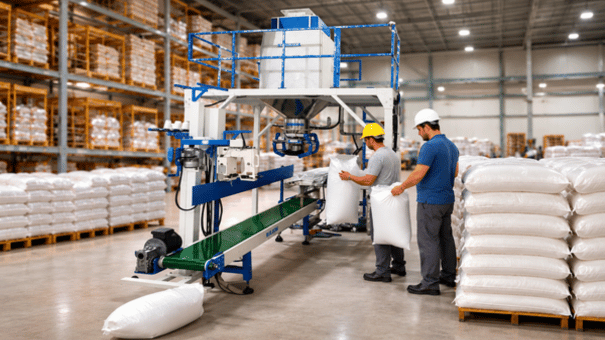
Chemical Packing Machine
The safe, accurate, and efficient packaging of chemicals is paramount across a multitude of industries. From granular fertilizers to liquid solvents and fine powders, the demands placed on packaging machinery are stringent. A reliable chemical packing machine is not merely a piece of equipment; it's a critical component in maintaining product integrity, ensuring workplace safety, and optimizing production output. Samirika Industries Pvt. Ltd. offers a comprehensive range of material handling and automation systems designed to meet these exacting standards for the chemical sector and beyond.
Understanding Chemical Packing Machines
Chemical packing machines are specifically engineered to handle a wide spectrum of chemical products, including liquids, powders, granules, and solids. Their primary function is to accurately fill, weigh, seal, and bag these substances into various containers, ensuring product containment and preventing contamination or spillage. Given the often hazardous or corrosive nature of chemical products, these machines are built with robust materials and precise control systems.
Key challenges in chemical packaging include managing corrosive or hazardous substances, achieving high dosing accuracy, handling viscosity variations and foaming, and ensuring compatibility with a diverse range of container types and sizes. Advanced chemical packaging machinery is designed to overcome these obstacles, incorporating features for precise measurements, secure sealing, and safe handling.
Applications of Chemical Packing Machines 📦
The versatility of chemical packing machines makes them indispensable across various sectors. Samirika Industries serves a broad range of industries with its material handling solutions, many of which are directly applicable to chemical packaging needs:
- Chemical Industry: Packaging of corrosive liquids, powders, granules, fertilizers, pesticides, and industrial chemicals. Machines must ensure containment and prevent hazardous material exposure.
- Polymer Industry: Efficiently packing polymer granules, pellets, and powders, often requiring high-volume capacity and dust control.
- Agriculture: Packaging of fertilizers, seeds, and soil conditioners, demanding accurate weighing and durable packaging.
- Minerals & Fuels: Handling and packaging of mineral powders, coal dust, and fuel additives, often in large formats like jumbo bags.
- Food & Animal Feed: While distinct from industrial chemicals, the principles of accurate weighing, hygienic filling, and secure sealing are shared for food-grade chemicals, additives, and animal feed ingredients.
These applications highlight the need for machinery that can adapt to different product forms, viscosities, and hazard levels, ensuring safe and reliable packaging operations.
Key Features of Advanced Chemical Packing Machinery
Selecting the right chemical packing machine involves considering several critical features that ensure performance, safety, and longevity:
- High Weighing and Filling Accuracy: Essential for precise dosing of both liquid and powder chemicals, minimizing product waste and ensuring compliance with product specifications.
- Robust Construction: Machines designed for chemical handling often require corrosion-resistant materials and sturdy frames to withstand harsh environments and heavy usage.
- Customization Capabilities: The ability to custom-build machines to meet specific industry requirements, including handling unique product characteristics or integrating with existing production lines.
- Safety Features: Including dust containment systems, emergency stop mechanisms, and, for flammable substances, explosion-proof (ExProof) capabilities.
- Ease of Operation and Maintenance: Intuitive controls and accessible components simplify operation and reduce downtime for cleaning and maintenance.
- Automation Integration: Seamless integration with other automated systems like bag placers, pushers, and checkweighers to create a fully automated packaging line.
Benefits of Investing in Quality Chemical Packing Equipment
Implementing high-quality chemical packing machines offers significant advantages for businesses:
- Enhanced Safety: Reduces manual handling of potentially hazardous materials, minimizing operator exposure and workplace accidents.
- Increased Production Output: Automated processes significantly speed up packaging operations, leading to higher throughput and efficiency.
- Improved Product Integrity: Precise filling and sealing prevent contamination, leakage, and product degradation, maintaining quality from production to end-user.
- Reduced Operational Costs: Minimizing product giveaway through accurate weighing, reducing labor requirements, and lowering downtime contributes to overall cost savings.
- Consistent Quality: Ensures uniform packaging across all products, enhancing brand consistency and customer satisfaction.
Choosing the Right Chemical Packing Machine: A Buyer's Guide
Selecting the appropriate chemical packing machine requires careful consideration of your specific needs. Samirika Industries Pvt. Ltd. can assist in identifying the best solutions from their range of material handling systems.
Key Considerations Before You Buy:
- Product Characteristics: Identify the physical state (liquid, powder, granule), viscosity, corrosiveness, flammability, and potential hazards of the chemicals to be packaged.
- Packaging Format: Determine the required container types (bags, bottles, drums, jumbo bags) and sizes.
- Required Accuracy: Define the acceptable tolerance for weight or volume filling.
- Production Volume: Estimate your current and future packaging needs to select a machine with adequate capacity and speed.
- Integration Needs: Consider how the new machine will fit into your existing production line and whether upstream or downstream automation is required.
- Safety Regulations: Ensure the machine complies with all relevant safety standards, especially for hazardous or flammable materials (e.g., ATEX compliance if applicable).
Buyer Insight:
Always consult with your potential supplier about the specific challenges your chemicals present. Customization is often key to ensuring a safe, efficient, and long-lasting solution. Understanding the material compatibility of the machine's components is crucial for handling corrosive substances.
Questions to Ask Potential Suppliers:
- Can this machine accurately handle the viscosity/flow rate of my product?
- What materials are used in the construction of the parts that contact the product?
- What level of automation can be integrated with this machine (e.g., automatic bag placing, pushing, sealing)?
- What are the maintenance requirements and recommended service intervals?
- Can you provide documentation on safety features and compliance?
- What are the options for customization to meet my specific chemical handling needs?
Samirika Industries: Your Partner in Material Handling & Automation
Samirika Industries Pvt. Ltd. specializes in providing comprehensive material handling systems with advanced automation. While serving diverse industries, their expertise in automatic weighing and bagging systems, polymer packaging machines, and jumbo packing machines directly addresses the core needs of chemical packaging. Their product portfolio also includes essential ancillary equipment such as automatic bag placers and pushers, belt conveyor systems, sealing machines, online checkweighers with rejection systems, and silos/hoppers. Located in Ahmedabad, Gujarat, Samirika Industries is strategically positioned to offer efficient solutions and support for businesses seeking to enhance their packaging operations with precision, reliability, and safety.
The company's commitment to automation extends to offering complete solutions designed to increase production output, improve line performance, and minimize manual handling. Whether your needs involve delicate powder filling or robust handling of granular materials, Samirika Industries provides the engineered systems to meet the challenge.
Frequently Asked Questions
What types of chemicals can be packaged using these machines?
Chemical packing machines can handle a wide variety, including liquids, powders, granules, corrosive substances, and hazardous materials. Specific machine designs often cater to the unique properties of each chemical type.
Are explosion-proof (ExProof) options available?
Yes, for handling flammable or explosive chemicals, specialized machines with ATEX – Explosion Proof (ExProof) capabilities are designed to ensure safety in hazardous environments.
How important is the material of construction for chemical packing machines?
Material of construction is critical, especially for corrosive chemicals. Stainless steel, specialized alloys, or chemically resistant coatings are often used to prevent degradation of the machine and contamination of the product.
Can these machines be integrated with existing production lines?
Absolutely. Industrial chemical packaging machinery is often designed for integration with other systems like conveyors, checkweighers, and cappers to create a seamless, automated workflow.
What role do checkweighers play in chemical packing?
Checkweighers are used to verify that each package contains the correct amount of product. Systems with rejection capabilities automatically remove underfilled or overfilled packages, ensuring accuracy and compliance.
Optimize Your Chemical Packaging Process Today
Enhance safety, efficiency, and accuracy in your chemical packaging operations. Explore how Samirika Industries Pvt. Ltd.'s advanced weighing, bagging, and material handling solutions can be tailored to your specific needs. Contact us to discuss your project requirements and receive a customized solution.
Samirika Industries Pvt. Ltd.
47, Paavan Industrial Park, opp. Shreenathji Ind Estate, Bakrol - Bujrang, Ahmedabad, Gujarat - 382430.
Phone: +91 9824393945
Email: sales@samirikagroup.in