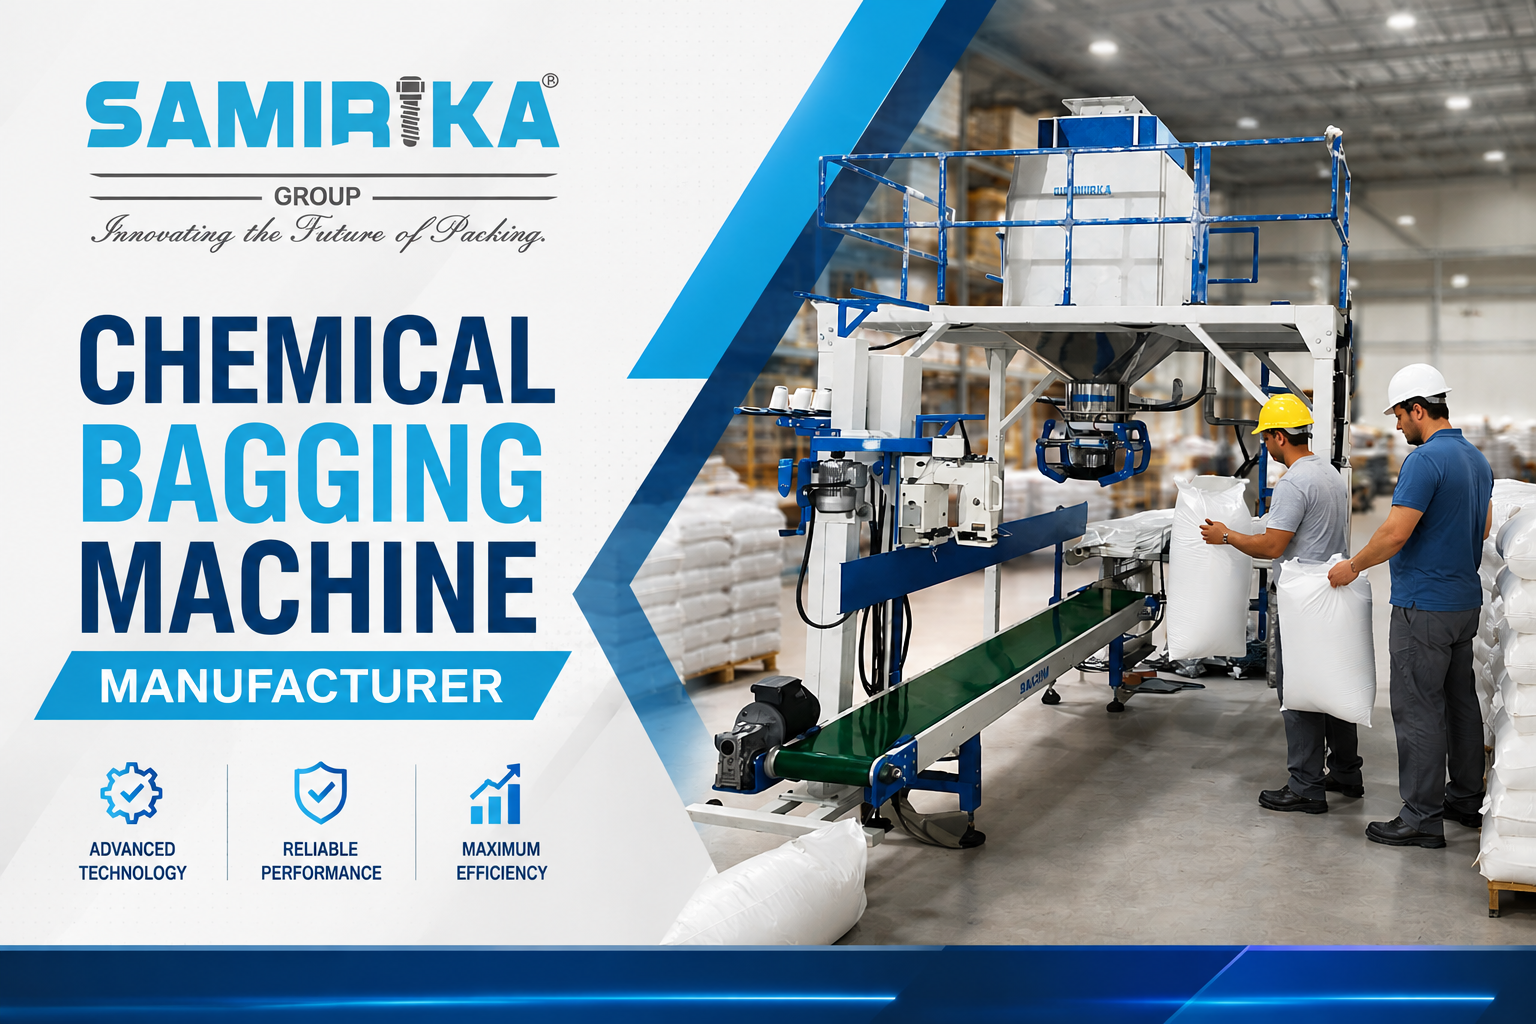
Chemical Bagging Machine Manufacturer
Expert chemical bagging machine manufacturer in Ahmedabad. Discover reliable, automated solutions for precise and efficient chemical packaging from Samirika Ind
What is a Chemical Bagging Machine? — Overview
A chemical bagging machine is an automated or semi-automated system designed to accurately fill and seal bags with various chemical products. These machines are engineered to handle a wide range of chemical forms, including powders, granules, pellets, and flakes, while ensuring precise weight dispensing and secure sealing. They are crucial for industries where accurate dosing, dust containment, and product protection are essential. Modern chemical bagging machines often incorporate advanced features like microprocessor-based controllers, integrated weighing systems, and dust collection mechanisms for enhanced performance and safety.
Key Features and Technical Specifications
When evaluating chemical bagging machines, several key features and technical specifications are vital for ensuring optimal performance and suitability for your specific chemical products and operational needs.
- Microprocessor-Based Controller: Provides precise control over filling, weighing, and sealing cycles, allowing for accurate adjustments and repeatable performance.
- Integrated Weighing System: Utilizes load cells or other precision weighing mechanisms to ensure each bag is filled to the exact target weight, minimizing product giveaway and ensuring consistency.
- Adjustable Filling Speed: Allows operators to modify the rate at which the product is dispensed into the bag, accommodating different product flow characteristics and bag sizes.
- Dust Containment System: Incorporates features like dust hoods, vacuum extraction, or enclosed filling nozzles to minimize airborne dust, protecting workers and the environment.
- Bag Sealing Options: Offers various sealing methods such as heat sealing, impulse sealing, or stitching, chosen based on the bag material and the chemical's properties.
- Durable Construction: Built with materials resistant to chemical corrosion and wear, ensuring longevity and reliability in demanding industrial environments.
- User-Friendly Interface: Features intuitive controls and displays for easy operation, monitoring, and troubleshooting.
- Customizable Hopper and Feeders: Adaptable to different product types and flow rates, ensuring smooth and consistent product delivery to the filling mechanism.
Industrial Applications and Use Cases
Chemical bagging machines are indispensable across a broad spectrum of industries that handle chemical products. Their versatility allows them to be adapted to specific material properties and packaging requirements.
- Fertilizer Packaging: Accurately filling bags with granular or powdered fertilizers, ensuring correct weight for agricultural applications.
- Detergent and Cleaning Agent Packaging: Handling powdered or granular detergents, soaps, and other cleaning chemicals with precise dosing and secure sealing.
- Agrochemical Packaging: Packaging pesticides, herbicides, and other agrochemicals in controlled environments to prevent contamination and ensure safety.
- Industrial Chemical Packaging: Filling bags with bulk industrial chemicals, pigments, dyes, and additives used in manufacturing processes.
- Polymer and Plastic Granule Packaging: Packaging plastic pellets, resins, and other polymer materials for distribution to manufacturing clients.
- Mineral and Ore Packaging: Filling bags with powdered or granular minerals, ores, and construction materials like cement or additives.
- Food Additive and Ingredient Packaging: While requiring specific food-grade standards, these machines can handle certain chemical food ingredients and additives.
- Pharmaceutical Ingredient Packaging: For non-sterile bulk chemical ingredients used in pharmaceutical manufacturing, requiring high precision and containment.
How to Choose the Right Chemical Bagging Machine
Selecting the appropriate chemical bagging machine is a crucial decision that impacts efficiency, safety, and cost-effectiveness. Consider these factors carefully:
- Product Characteristics: What is the physical form of your chemical (powder, granule, flake)? What is its flowability, density, and abrasiveness? Does it require special handling due to corrosiveness or reactivity?
- Bag Type and Size: What type of bags will you use (e.g., multi-wall paper, woven PP, plastic film)? What are the required bag dimensions and fill weights?
- Accuracy and Speed Requirements: What level of weighing accuracy is critical for your product and market? What is your desired production output per hour or shift?
- Automation Level: Do you need a fully automatic system, or will a semi-automatic solution suffice? Consider labor availability and operational workflow.
- Dust Control and Safety Features: Given the nature of chemicals, robust dust containment and safety interlocks are essential. What level of dust extraction is needed?
- Material Compatibility: Ensure the machine's construction materials are compatible with your specific chemicals to prevent corrosion and contamination.
- Supplier Support and Service: Look for a manufacturer with a strong reputation for after-sales service, spare parts availability, and technical support, especially for critical industrial equipment.
- Certifications and Compliance: Verify that the machine meets relevant industry standards and safety regulations for chemical handling.
Quality Standards and Compliance
For chemical bagging machines, adherence to stringent quality standards and regulatory compliance is non-negotiable. Manufacturers like Samirika Industries Pvt. Ltd. prioritize these aspects to ensure the safety, reliability, and efficacy of their equipment. Key standards and compliance factors to look for include:
ISO Certifications: ISO 9001 for quality management systems demonstrates a commitment to consistent product quality and customer satisfaction.
Electrical Safety Standards: Compliance with standards such as IEC (International Electrotechnical Commission) or relevant national standards ensures electrical components and systems are safe to operate.
Material Handling Standards: While specific chemical bagging machine standards might vary, general principles of robust design, material compatibility, and operational safety are paramount.
Environmental Regulations: Machines should be designed to minimize dust emissions and comply with local environmental protection guidelines.
ATEX Compliance (if applicable): For chemicals that pose an explosion risk, equipment may need to comply with ATEX directives for use in potentially explosive atmospheres.
Buyers should always verify the certifications and compliance documentation provided by the manufacturer and ensure the equipment meets the specific safety and operational requirements for their chemical products and facility.
Why Samirika Industries' Experience and Capability Matters
At Samirika Industries Pvt. Ltd., our extensive experience in designing and manufacturing material handling and packaging automation systems, particularly for demanding sectors like the chemical industry, sets us apart. Our Ahmedabad-based facility is equipped with advanced manufacturing capabilities, allowing us to engineer robust, precise, and reliable chemical bagging machines. Our team comprises experienced engineers and technicians who understand the unique challenges of handling diverse chemical products.
We focus on a meticulous manufacturing process, ensuring that every machine undergoes rigorous quality control checks. This dedication to quality, combined with our ability to provide customized solutions tailored to specific client needs, ensures that our customers receive equipment that enhances their operational efficiency and safety. Our commitment extends beyond delivery, with comprehensive after-sales support and a focus on building long-term partnerships with our clients.
Installation, Maintenance, and Care Tips
Proper installation, regular maintenance, and careful operation are crucial for the longevity and optimal performance of your chemical bagging machine.
- Installation: Ensure the machine is installed on a stable, level surface. Connect all utilities (power, compressed air if applicable) according to the manufacturer's specifications. Calibrate the weighing system accurately before initial operation.
- Regular Cleaning: After each production run, thoroughly clean the machine, especially the filling spout, weighing hopper, and sealing area. Use appropriate cleaning agents that are compatible with both the machine materials and the chemicals handled.
- Lubrication: Follow the manufacturer's lubrication schedule for all moving parts to ensure smooth operation and prevent premature wear.
- Inspection of Wear Parts: Periodically inspect components like sealing jaws, belts, and filling augers for signs of wear. Replace them promptly to maintain sealing integrity and filling accuracy.
- Calibration Checks: Regularly verify the accuracy of the weighing system. Recalibrate as needed, especially if product characteristics change or after significant maintenance.
- Dust System Maintenance: Ensure dust collection filters are clean and the vacuum system is functioning efficiently to maintain a safe working environment.
- Operator Training: Properly train all operators on the machine's functions, safety features, and routine maintenance procedures.
Frequently Asked Questions
Our chemical bagging machines are designed to handle a wide array of chemical products, including powders, granules, pellets, and flakes. We engineer solutions for materials ranging from fine powders like pigments and detergents to granular products like fertilizers and polymers, ensuring compatibility and safe handling for each specific substance.
Our machines incorporate high-precision weighing systems, typically utilizing advanced load cells and microprocessor controllers. This allows for exceptional accuracy, often achieving a tolerance of +/- 0.5% to 1% of the target fill weight, depending on the product characteristics and machine configuration.
Safety is paramount. Our machines are equipped with features such as emergency stop buttons, safety interlocks on access doors, dust containment systems with efficient extraction, and robust construction to prevent leaks. For specific hazardous chemicals, we can incorporate additional safety measures and ATEX-compliant components.
Yes, our chemical bagging machines are often designed with flexibility in mind. We can configure them to accommodate a range of bag sizes and types, including multi-wall paper bags, woven polypropylene bags, and plastic film bags, with adjustments for different sealing methods like heat sealing or stitching.
We offer comprehensive after-sales support, including installation assistance, operator training, readily available spare parts, and prompt technical assistance. Our goal is to ensure your equipment operates efficiently and reliably throughout its lifespan.
We select appropriate construction materials, such as specific grades of stainless steel (e.g., SS304, SS316) or specialized coatings, based on the chemical properties of the products being handled. This ensures the machine's durability and prevents contamination or degradation over time.
Conclusion
For chemical manufacturers in Ahmedabad and beyond, investing in a high-quality, reliable chemical bagging machine is a strategic decision that directly influences operational efficiency, product integrity, and workplace safety. Understanding the specific requirements of your chemical products, desired output, and necessary safety features is key to selecting the right equipment. Partnering with an experienced manufacturer like Samirika Industries Pvt. Ltd., known for its engineering expertise, quality manufacturing, and commitment to customer support, ensures you receive a tailored solution that meets stringent industry demands and contributes to your business's success.
Get In Touch
Samirika Industries Pvt. Ltd.