50 Kg Chemical Packing Machine
Optimize chemical packaging in Ahmedabad with advanced 50 Kg machines. Ensure precision, safety, and efficiency for powders and granules.
Why This Matters in Ahmedabad, Gujarat
Ahmedabad and the broader Gujarat region stand as a significant hub for chemical manufacturing, processing, and distribution. Industries ranging from petrochemicals and agrochemicals to specialty chemicals and pharmaceuticals have a strong presence here. This industrial landscape creates a constant demand for advanced packaging solutions that can handle diverse chemical properties, from fine powders to granular materials. Companies in Ahmedabad require packaging systems that can keep pace with production volumes, meet stringent quality controls, and adapt to evolving market needs, making the selection of a reliable 50 Kg chemical packing machine a strategic business decision.
What is a 50 Kg Chemical Packing Machine — Overview
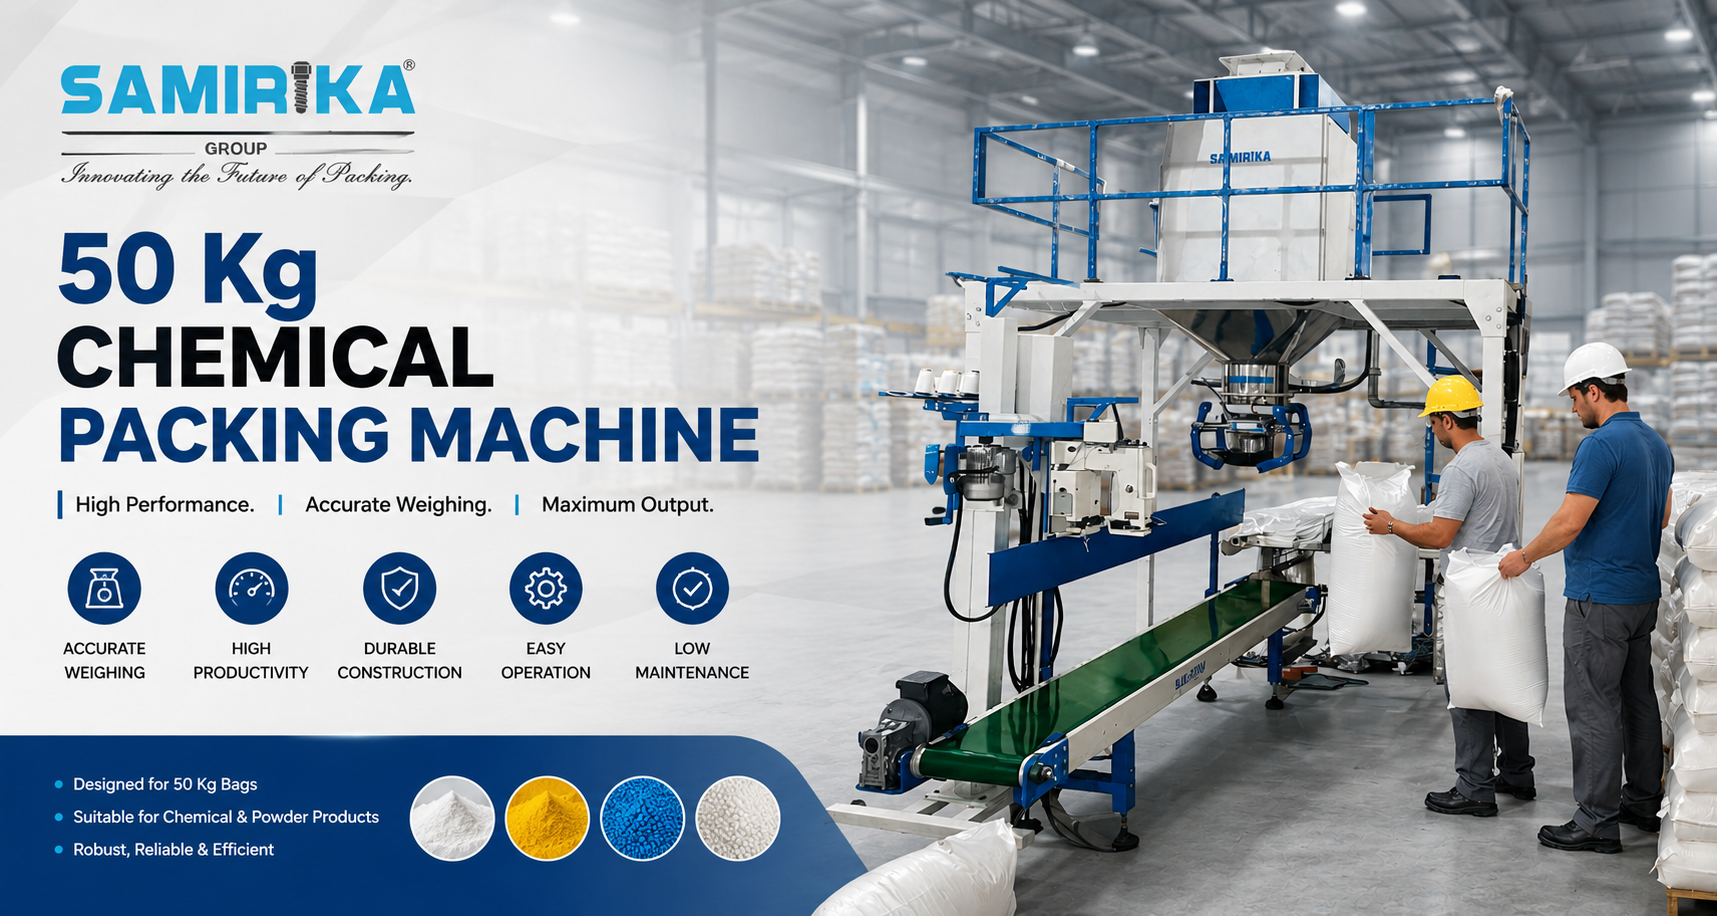
A 50 Kg chemical packing machine is an automated or semi-automated system designed to accurately weigh, fill, and seal chemical products into 50-kilogram bags or sacks. These machines typically utilize advanced weighing technology, such as load cells, to ensure precise dosing, minimizing product giveaway and ensuring consistency. They are engineered to handle various material characteristics, including corrosive, abrasive, or dusty chemicals, often incorporating features for dust suppression and material-specific handling. The core function is to streamline the packaging process, moving from manual labor to a more efficient, safer, and accurate automated operation.
Key Features and Technical Specifications
- High-Precision Load Cells: Ensures accurate weighing of chemical products, typically within +/- 0.1% to 0.2% tolerance.
- Corrosion-Resistant Contact Parts: Constructed from stainless steel or specialized alloys to withstand aggressive chemical environments.
- Microprocessor-Based Control System: Offers programmable settings for different product types and bag weights, enhancing operational flexibility.
- Integrated Dust Collection System: Minimizes airborne particles during filling, improving workplace safety and cleanliness.
- Adjustable Bag Clamping Mechanism: Securely holds various bag types and sizes, preventing spills and ensuring proper filling.
- Vibration Feeders or Screw Feeders: Optimized for consistent material flow, whether for free-flowing granules or cohesive powders.
- User-Friendly Human-Machine Interface (HMI): Simplifies operation, monitoring, and troubleshooting for operators.
- Robust and Durable Construction: Engineered for continuous industrial operation with minimal downtime.
Industrial Applications and Use Cases
- Fertilizer Manufacturing: Packaging granular and powdered fertilizers for agricultural distribution.
- Pigment and Dye Production: Handling fine chemical powders used in paints, textiles, and plastics.
- Industrial Salt Processing: Bagging various grades of industrial salts for water treatment, food processing, and chemical synthesis.
- Construction Chemical Blending: Packaging cement additives, tile adhesives, and other dry mix construction materials.
- Polymer and Resin Production: Filling plastic granules, pellets, and powdered resins for manufacturing.
- Agrochemical Formulation: Packaging pesticides, herbicides, and other crop protection chemicals.
- Mineral Processing: Bagging processed minerals like bentonite, silica, or calcium carbonate.
How to Choose the Right 50 Kg Chemical Packing Machine
Selecting the appropriate 50 Kg chemical packing machine requires careful consideration of several factors to ensure it meets specific operational demands and long-term business goals. A thorough evaluation helps prevent costly mismatches and ensures optimal performance.
- Material Characteristics: Assess the chemical's properties (corrosive, abrasive, dusty, hygroscopic, flowability) to ensure material compatibility and appropriate feeder type.
- Required Throughput: Determine the desired bags per hour to match machine capacity with production targets.
- Accuracy Requirements: Verify the machine's weighing precision to meet product specifications and minimize material giveaway.
- Automation Level: Decide between semi-automatic (operator places bags) or fully automatic (integrated bag placers) based on labor availability and production scale.
- Safety Features: Look for integrated safety interlocks, dust control, and explosion-proof components if handling hazardous chemicals.
- Integration Capability: Consider how easily the machine can integrate with existing upstream (silos, conveyors) and downstream (sealing, palletizing) equipment.
- Supplier Experience and Support: Evaluate the manufacturer's track record, technical expertise, and availability of after-sales service and spare parts.
- Certifications and Compliance: Ensure the machine adheres to relevant industry standards and safety regulations.
Quality Standards and Compliance
Adherence to quality standards and compliance is non-negotiable when dealing with chemical packing machinery. Buyers should verify that the 50 Kg chemical packing machine meets international and national standards such as ISO 9001 for quality management systems, which indicates a commitment to consistent product quality. For electrical components, IEC standards are crucial. Furthermore, depending on the specific chemicals being handled, compliance with safety directives like ATEX (for potentially explosive atmospheres) may be essential. Reputable suppliers will provide documentation and certifications, demonstrating their equipment's reliability, safety, and performance. Verifying these standards before procurement helps ensure operational safety and regulatory adherence.
Why Samirika Industries Pvt. Ltd. Experience and Capability Matters
Samirika Industries Pvt. Ltd. brings extensive experience in delivering comprehensive material handling and packaging automation solutions, including specialized 50 Kg chemical packing machines. Our approach focuses on precision engineering and robust construction, ensuring that each machine is built for durability and consistent performance in demanding chemical environments. We integrate fully automatic microprocessor-based controllers, allowing for highly accurate weighing and efficient bagging operations. Our technical team possesses deep knowledge of various chemical properties, enabling us to customize solutions that address specific material handling challenges, from corrosive powders to fine granules. We prioritize customer-centric service, providing reliable after-sales support and ensuring our systems enhance productivity, accuracy, and safety for our clients in Ahmedabad and beyond.
Installation, Maintenance and Care Tips
Proper installation and ongoing maintenance are crucial for the longevity and optimal performance of a 50 Kg chemical packing machine. Ensure the machine is installed on a level, stable foundation capable of supporting its weight and operational vibrations. Initial calibration by qualified technicians is essential to guarantee weighing accuracy.
- Regular Cleaning: Clean all contact parts daily, especially when handling corrosive or sticky chemicals, to prevent buildup and maintain hygiene.
- Lubrication Schedule: Follow the manufacturer's guidelines for lubricating moving parts to reduce wear and tear.
- Component Inspection: Periodically inspect load cells, sensors, belts, and pneumatic components for signs of wear, damage, or misalignment.
- Software Updates: Keep the control system software updated to benefit from performance improvements and bug fixes.
- Operator Training: Ensure all operators are thoroughly trained on the machine's operation, safety protocols, and basic troubleshooting.
- Spare Parts Inventory: Maintain an inventory of critical spare parts to minimize downtime during unexpected component failures.
Frequently Asked Questions
These machines are engineered to handle a wide range of chemical products, including powders, granules, flakes, and pellets. This includes materials like fertilizers, industrial salts, pigments, resins, construction chemicals, and various agrochemicals. The machine's contact parts are typically constructed from corrosion-resistant materials to ensure compatibility with diverse chemical properties.
Modern 50 Kg chemical packing machines utilize advanced load cell technology and microprocessor-based control systems to achieve high levels of accuracy. Typically, they can maintain a weighing tolerance of +/- 0.1% to 0.2% of the target weight. This precision helps minimize product giveaway and ensures consistent bag weights, which is crucial for quality control and cost efficiency.
Safety is paramount in chemical handling. Common safety features include integrated dust collection systems to reduce airborne particles, safety interlocks on access doors, emergency stop buttons, and robust guarding around moving parts. For hazardous chemicals, machines can be designed with explosion-proof components and ATEX compliance to prevent ignition risks.
Yes, most 50 Kg chemical packing machines are designed for seamless integration into existing material handling systems. They can be connected with upstream equipment like silos, hoppers, and conveyors, and downstream systems such as bag stitching or sealing machines, checkweighers, and robotic palletizers. This modular design allows for flexible system expansion and automation.
The throughput capacity varies significantly based on the machine's design, the chemical's flow properties, and the level of automation. Semi-automatic machines might pack 6-10 bags per minute, while fully automatic systems with integrated bag placers can achieve higher rates, often ranging from 12 to 20 bags per minute or more under optimal conditions.
Routine maintenance is essential for operational reliability. This typically involves daily cleaning of contact surfaces, regular lubrication of moving parts, and periodic inspection of load cells, sensors, and pneumatic components. Following the manufacturer's preventative maintenance schedule, including checking electrical connections and replacing worn parts, helps ensure long-term performance and minimize downtime.
Conclusion
The demand for efficient, accurate, and safe chemical packaging solutions in Ahmedabad, Gujarat, continues to grow. A reliable 50 Kg chemical packing machine is a foundational investment for any chemical manufacturer aiming to optimize their operations. By carefully considering factors such as material characteristics, required throughput, accuracy, and the supplier's experience, businesses can select equipment that not only meets their immediate needs but also supports long-term growth and compliance. Partnering with a capable manufacturer ensures access to robust technology, expert support, and solutions tailored to the unique challenges of chemical material handling.
Get In Touch
Samirika Industries Pvt. Ltd.